
 English
 Russian
 French
 Spanish
 Portuguese
 Korean
 Japanese
 Thai
Elevating Product Quality: Top 10 Benefits of Using a Vacuum Homogenizer Mixer
In modern industrial production, especially in industries that demand high precision, ultra-fine texture, and stable product consistency, the vacuum homogenizer mixer has evolved from a niche specialized equipment into a core production tool that cannot be ignored. Unlike traditional atmospheric mixing equipment, it integrates multiple core capabilities such as vacuum negative pressure control, high-shear homogenization, temperature precision regulation, and multi-form stirring. It can efficiently complete a series of complex operations including material mixing, dispersing, emulsifying, and deaeration in a closed environment. This not only solves many common pain points in traditional mixing processes but also builds a more solid foundation for enterprises to achieve quality breakthroughs and gain competitive advantages in the high-end market.
1. Eliminates Air Bubbles for a Flawless, Smooth Final Texture
One of the most intuitive and significant advantages of a vacuum homogenizer mixer is its powerful deaeration capability. During the mixing process, the equipment operates in a continuous negative pressure environment, which can quickly extract the tiny bubbles that are easily trapped in high-viscosity materials such as creams, ointments, and adhesives. This effectively avoids common defects such as pinholes, pores, and uneven surfaces in the final product. For high-end cosmetics, medical ointments, and optical-grade adhesives, the absence of bubbles directly means a more delicate and smooth product appearance, significantly enhancing the user's sensory experience and product added value.
2. Prevents Oxidation and Extends Product Shelf Life
Many sensitive raw materials such as active pharmaceutical ingredients, natural plant extracts, and unsaturated oils are prone to oxidative discoloration, deterioration, or performance degradation when exposed to air during mixing. The vacuum homogenizer mixer can discharge most of the air in the mixing chamber before the material is put in, creating an oxygen-deficient or even near-oxygen-free closed environment. This greatly reduces the probability of chemical reactions between materials and oxygen, effectively maintains the activity and stability of raw materials, and thus significantly extends the shelf life of the finished product. For the pharmaceutical and food industries, this means fewer preservatives can be used while ensuring safety, making products more in line with high-quality and healthy market demands.
3. Achieves Ultra-Fine, Uniform Particle Size Distribution
Equipped with a high-speed rotating homogenizing head and a precision-engineered shear gap, the vacuum homogenizer mixer can instantly break material particles from the micron level down to the submicron or even nanometer level under the dual action of vacuum negative pressure and high shear force. Compared with ordinary mixers, its particle size distribution is narrower and more uniform, and there will be no large particle agglomerates that are difficult to disperse. This performance is crucial for products such as pharmaceutical emulsions, ink pigments, and nano-coatings, as it directly determines the stability of the product and the uniformity of the final use effect.
4. Delivers Consistent Batch-to-Batch Production Quality
Traditional open mixing processes are easily affected by environmental temperature, humidity, manual operation differences, and material feeding sequences, leading to obvious quality fluctuations between different batches of products. The vacuum homogenizer mixer adopts a fully enclosed automated control system, which can precisely lock multiple core parameters such as vacuum degree, homogenization speed, stirring time, and reaction temperature. Each batch of materials can be mixed and processed under exactly the same conditions, ensuring that the quality indicators of different batches of finished products are highly consistent. This is particularly important for enterprises that have passed strict certifications such as GMP and ISO, helping them easily meet the strict requirements of large-scale standardized production.
5. Reduces Material Waste and Improves Production Yield
Under the vacuum condition, the fluidity and dispersion of materials are greatly enhanced, which can effectively reduce the residue of high-viscosity materials on the inner wall of the kettle and the surface of the stirring paddle. At the same time, the efficient and thorough mixing effect avoids the rework and material scrapping problems caused by uneven mixing and unqualified deaeration in the traditional process. Enterprises can obtain more qualified finished products with the same amount of raw materials, the production yield is significantly improved, and the raw material cost per unit of product is effectively reduced, bringing more considerable cost control benefits to large-scale continuous production.
6. Supports Gentle Processing for Heat-Sensitive Ingredients
Many active ingredients such as vitamins, biological enzymes, and protein components are extremely sensitive to high temperatures, and high temperatures for a long time will lead to inactivation and failure. The vacuum homogenizer mixer is usually equipped with a jacket heat exchange system. Under the vacuum negative pressure environment, the boiling point of the material will decrease, which can realize efficient mixing and emulsification at a relatively low temperature. It avoids the thermal damage of high-shear friction heat to heat-sensitive ingredients, maximizes the biological activity and functional characteristics of raw materials, and makes the product efficacy more prominent.
7. Minimizes Cross-Contamination for Higher Hygiene Standards
The equipment body of the vacuum homogenizer mixer is mostly made of high-grade stainless steel that meets hygiene standards. The inner wall is precisely polished without dead corners, which is convenient for CIP online cleaning and SIP high-temperature sterilization. The fully closed vacuum system completely isolates the materials from the external dust, microorganisms, and impurities in the air, avoiding the risk of cross-contamination that is easily caused by open operation. This design fully meets the strict hygiene requirements of the pharmaceutical, infant food, and high-end cosmetics industries, helping enterprises easily pass the most stringent production environment audits.
8. Cuts Down Processing Time and Boosts Production Efficiency
The vacuum homogenizer mixer integrates multiple functions such as stirring, homogenizing, emulsifying, deaerating, and heating into one equipment. It does not require multiple transfers and repeated processing of materials between different equipment. The high-shear homogenization under vacuum can complete the particle refinement and uniform mixing process in a very short time, which is several times or even ten times higher than the processing efficiency of traditional processes. The production cycle of a single batch is greatly shortened, which directly improves the overall production capacity of the production line and helps enterprises quickly respond to large orders in the market.
9. Enables Customization for Complex, High-Viscosity Formulations
Modern new product R&D and production often face a large number of complex high-viscosity formulations, such as dental impression materials, high-temperature-resistant sealants, and special functional ointments. The vacuum homogenizer mixer can be configured with a variety of stirring forms such as anchor type, screw belt type, double planetary type, and top homogenizing head according to the characteristics of the material. It can freely adjust the speed ratio of low-speed stirring and high-speed homogenization, and easily cope with various high-viscosity, easy-to-agglomerate, and difficult-to-disperse special materials. It provides flexible and reliable production possibilities for enterprises to develop high value-added new products.
10. Improves Operational Safety and Reduces Labor Intensity
The fully enclosed vacuum operation mode avoids the volatilization of harmful solvents, odors, and dust in the production workshop, creating a safer and more friendly working environment for operators. The automated control system can realize one-click start-up and preset program operation. Operators do not need to be exposed to high-risk material handling processes for a long time, and the labor intensity is greatly reduced. At the same time, the equipment is equipped with multiple safety interlock protections such as vacuum overload, over-temperature alarm, and pressure relief protection, which effectively avoids safety accidents in the production process and helps enterprises realize safer and more civilized production management.
From solving the most basic bubble and oxidation problems to realizing full-parameter precise control, efficient production, and flexible customized processing, the vacuum homogenizer mixer is not just a simple mixing equipment upgrade. It is a key tool for enterprises to move from ordinary production to high-end manufacturing and win the market with quality. For any production scenario that pursues ultimate product performance and stable quality, it is a core investment that can bring long-term and considerable returns.
News
- Latest News
- Solutions
- FAQ
Recommend Products
-
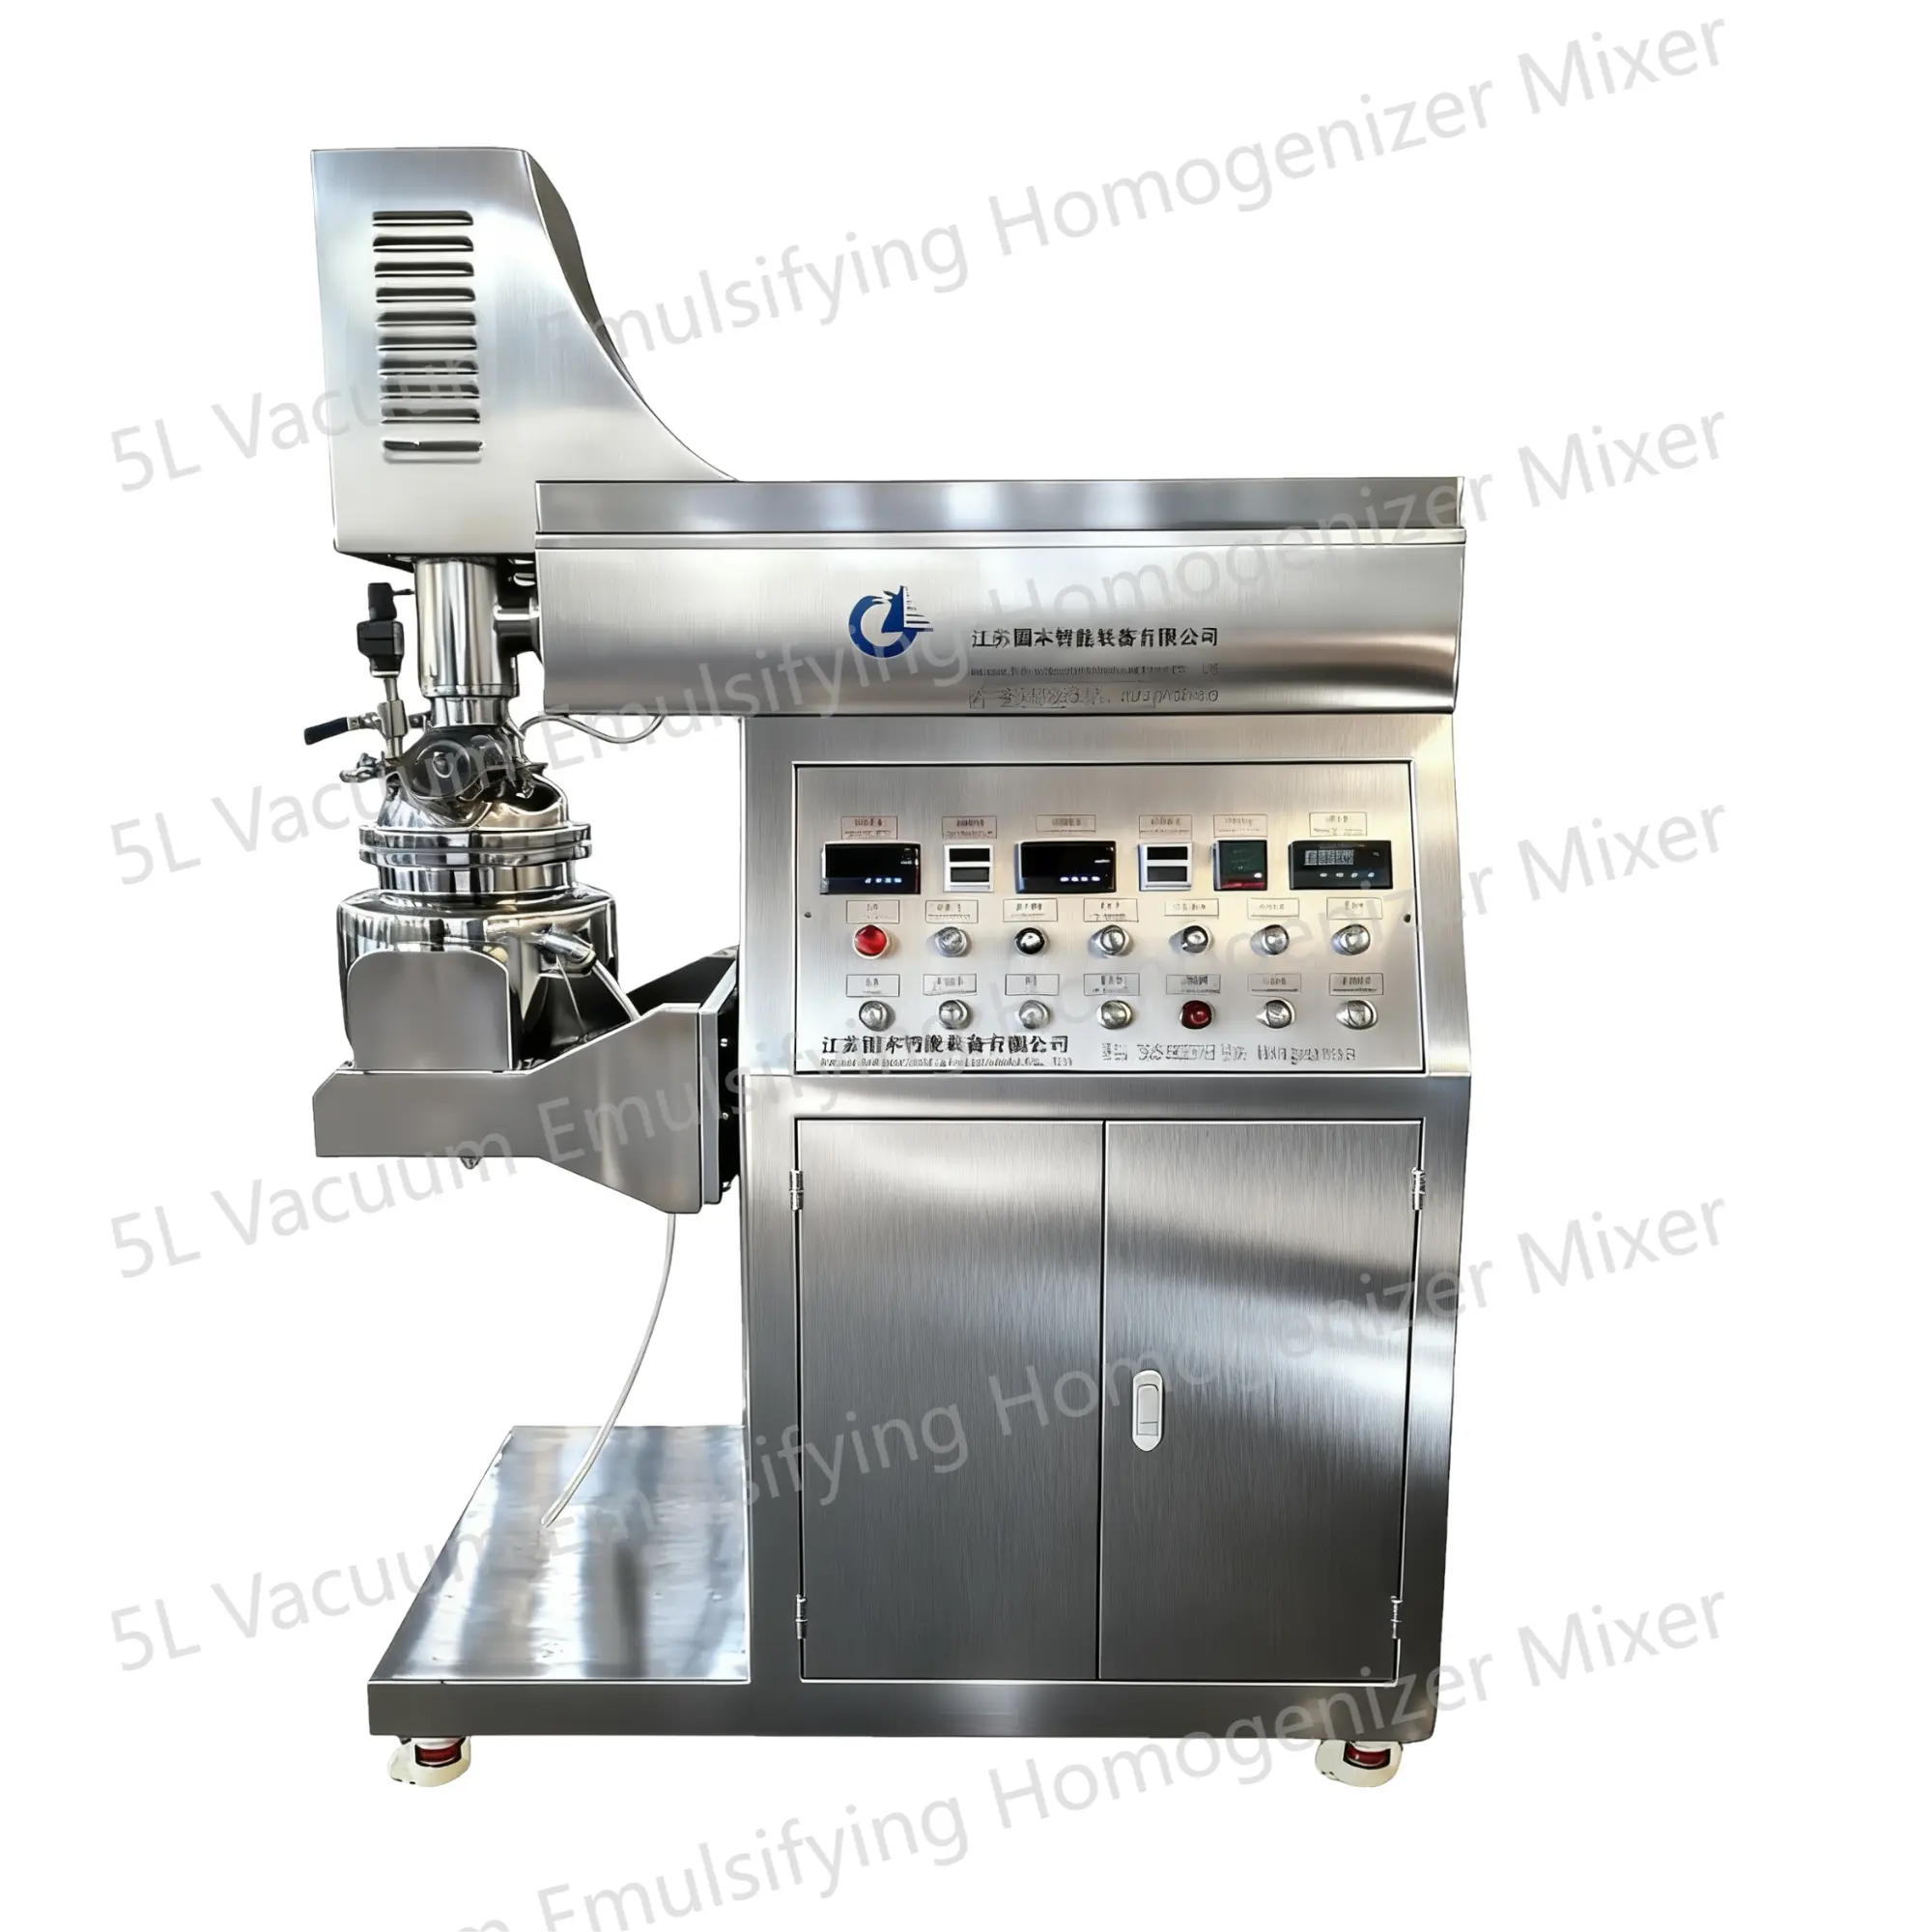 5L Vacuum Emulsifying Homogenizer Mixer
The 5L vacuum emulsifying mixer is a device designed for emulsifying and mixing various substances in a vacuum environment. This equipment is equipped with a mixing tank with a capacity of 5 liters and is widely applied in industries such as food, pharmaceuticals, cosmetics, and pesticides.
-
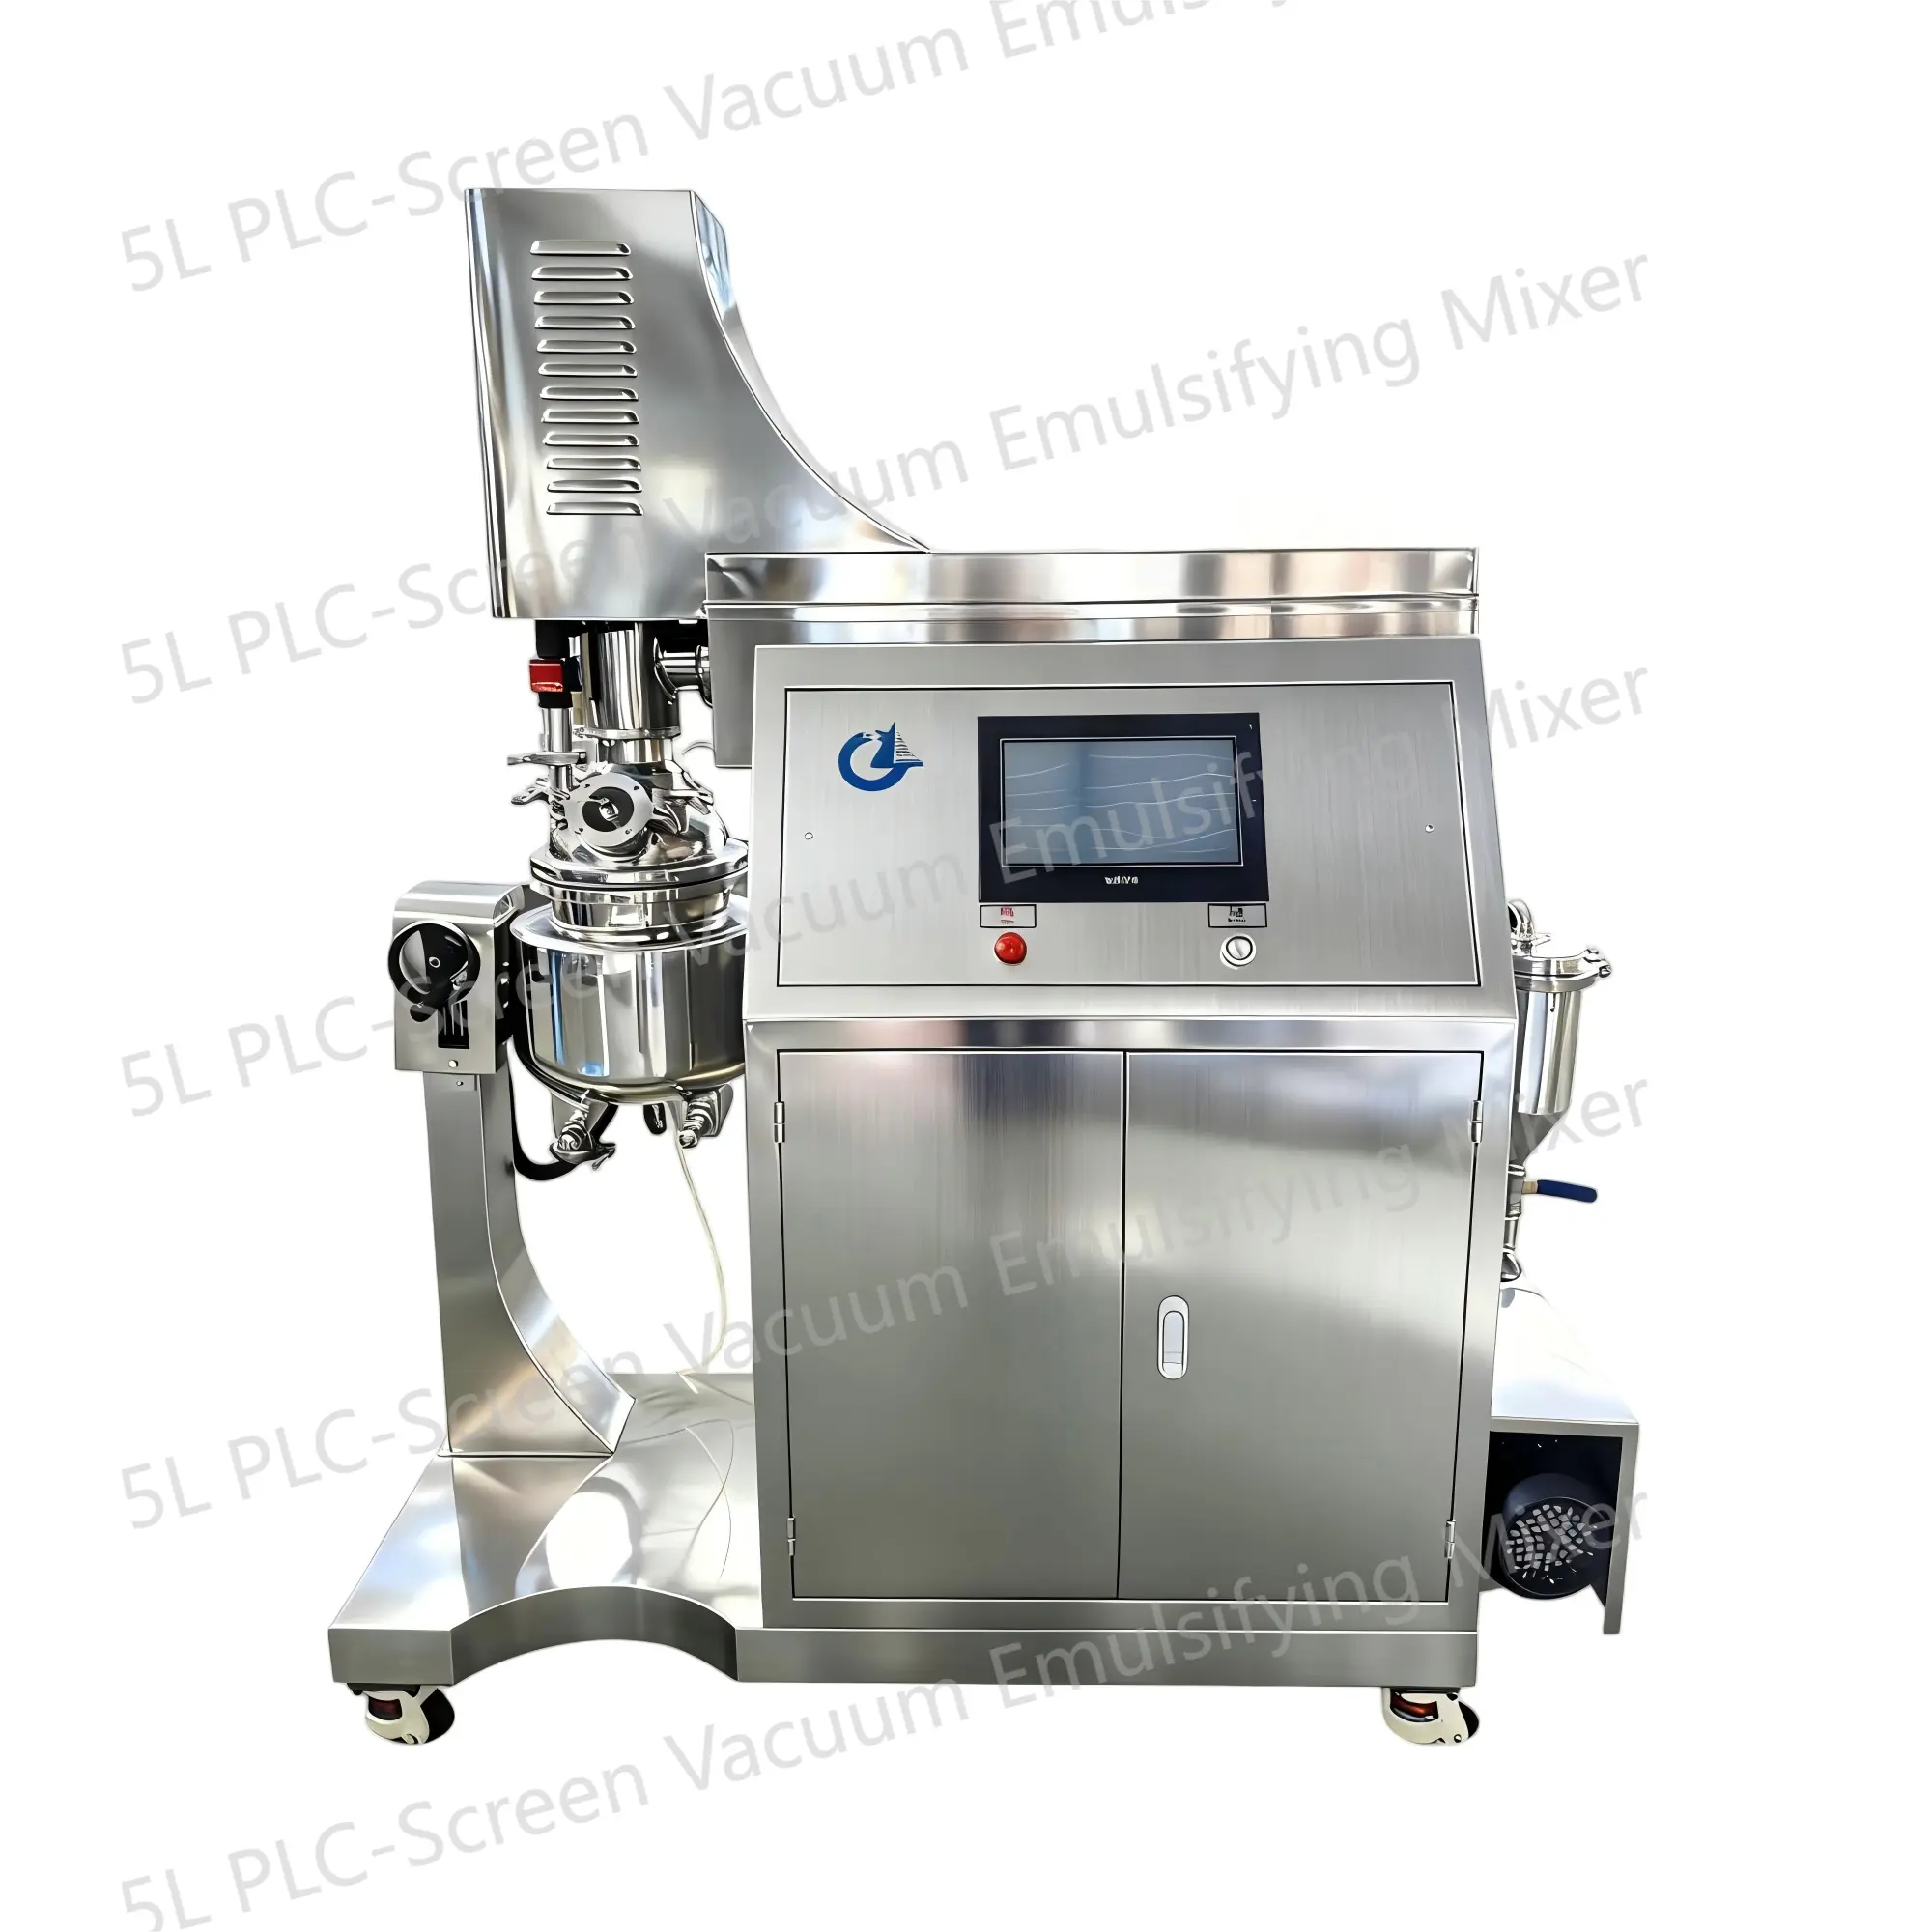 5L PLC-Screen Vacuum Emulsifying Mixer
The 5L PLC-Screen Vacuum Emulsifying Mixer is a device designed for emulsifying and mixing various substances in a vacuum environment. This equipment is equipped with a mixing tank with a capacity of 5 liters and is widely applied in industries such as food, pharmaceuticals, cosmetics, and pesticides.
-
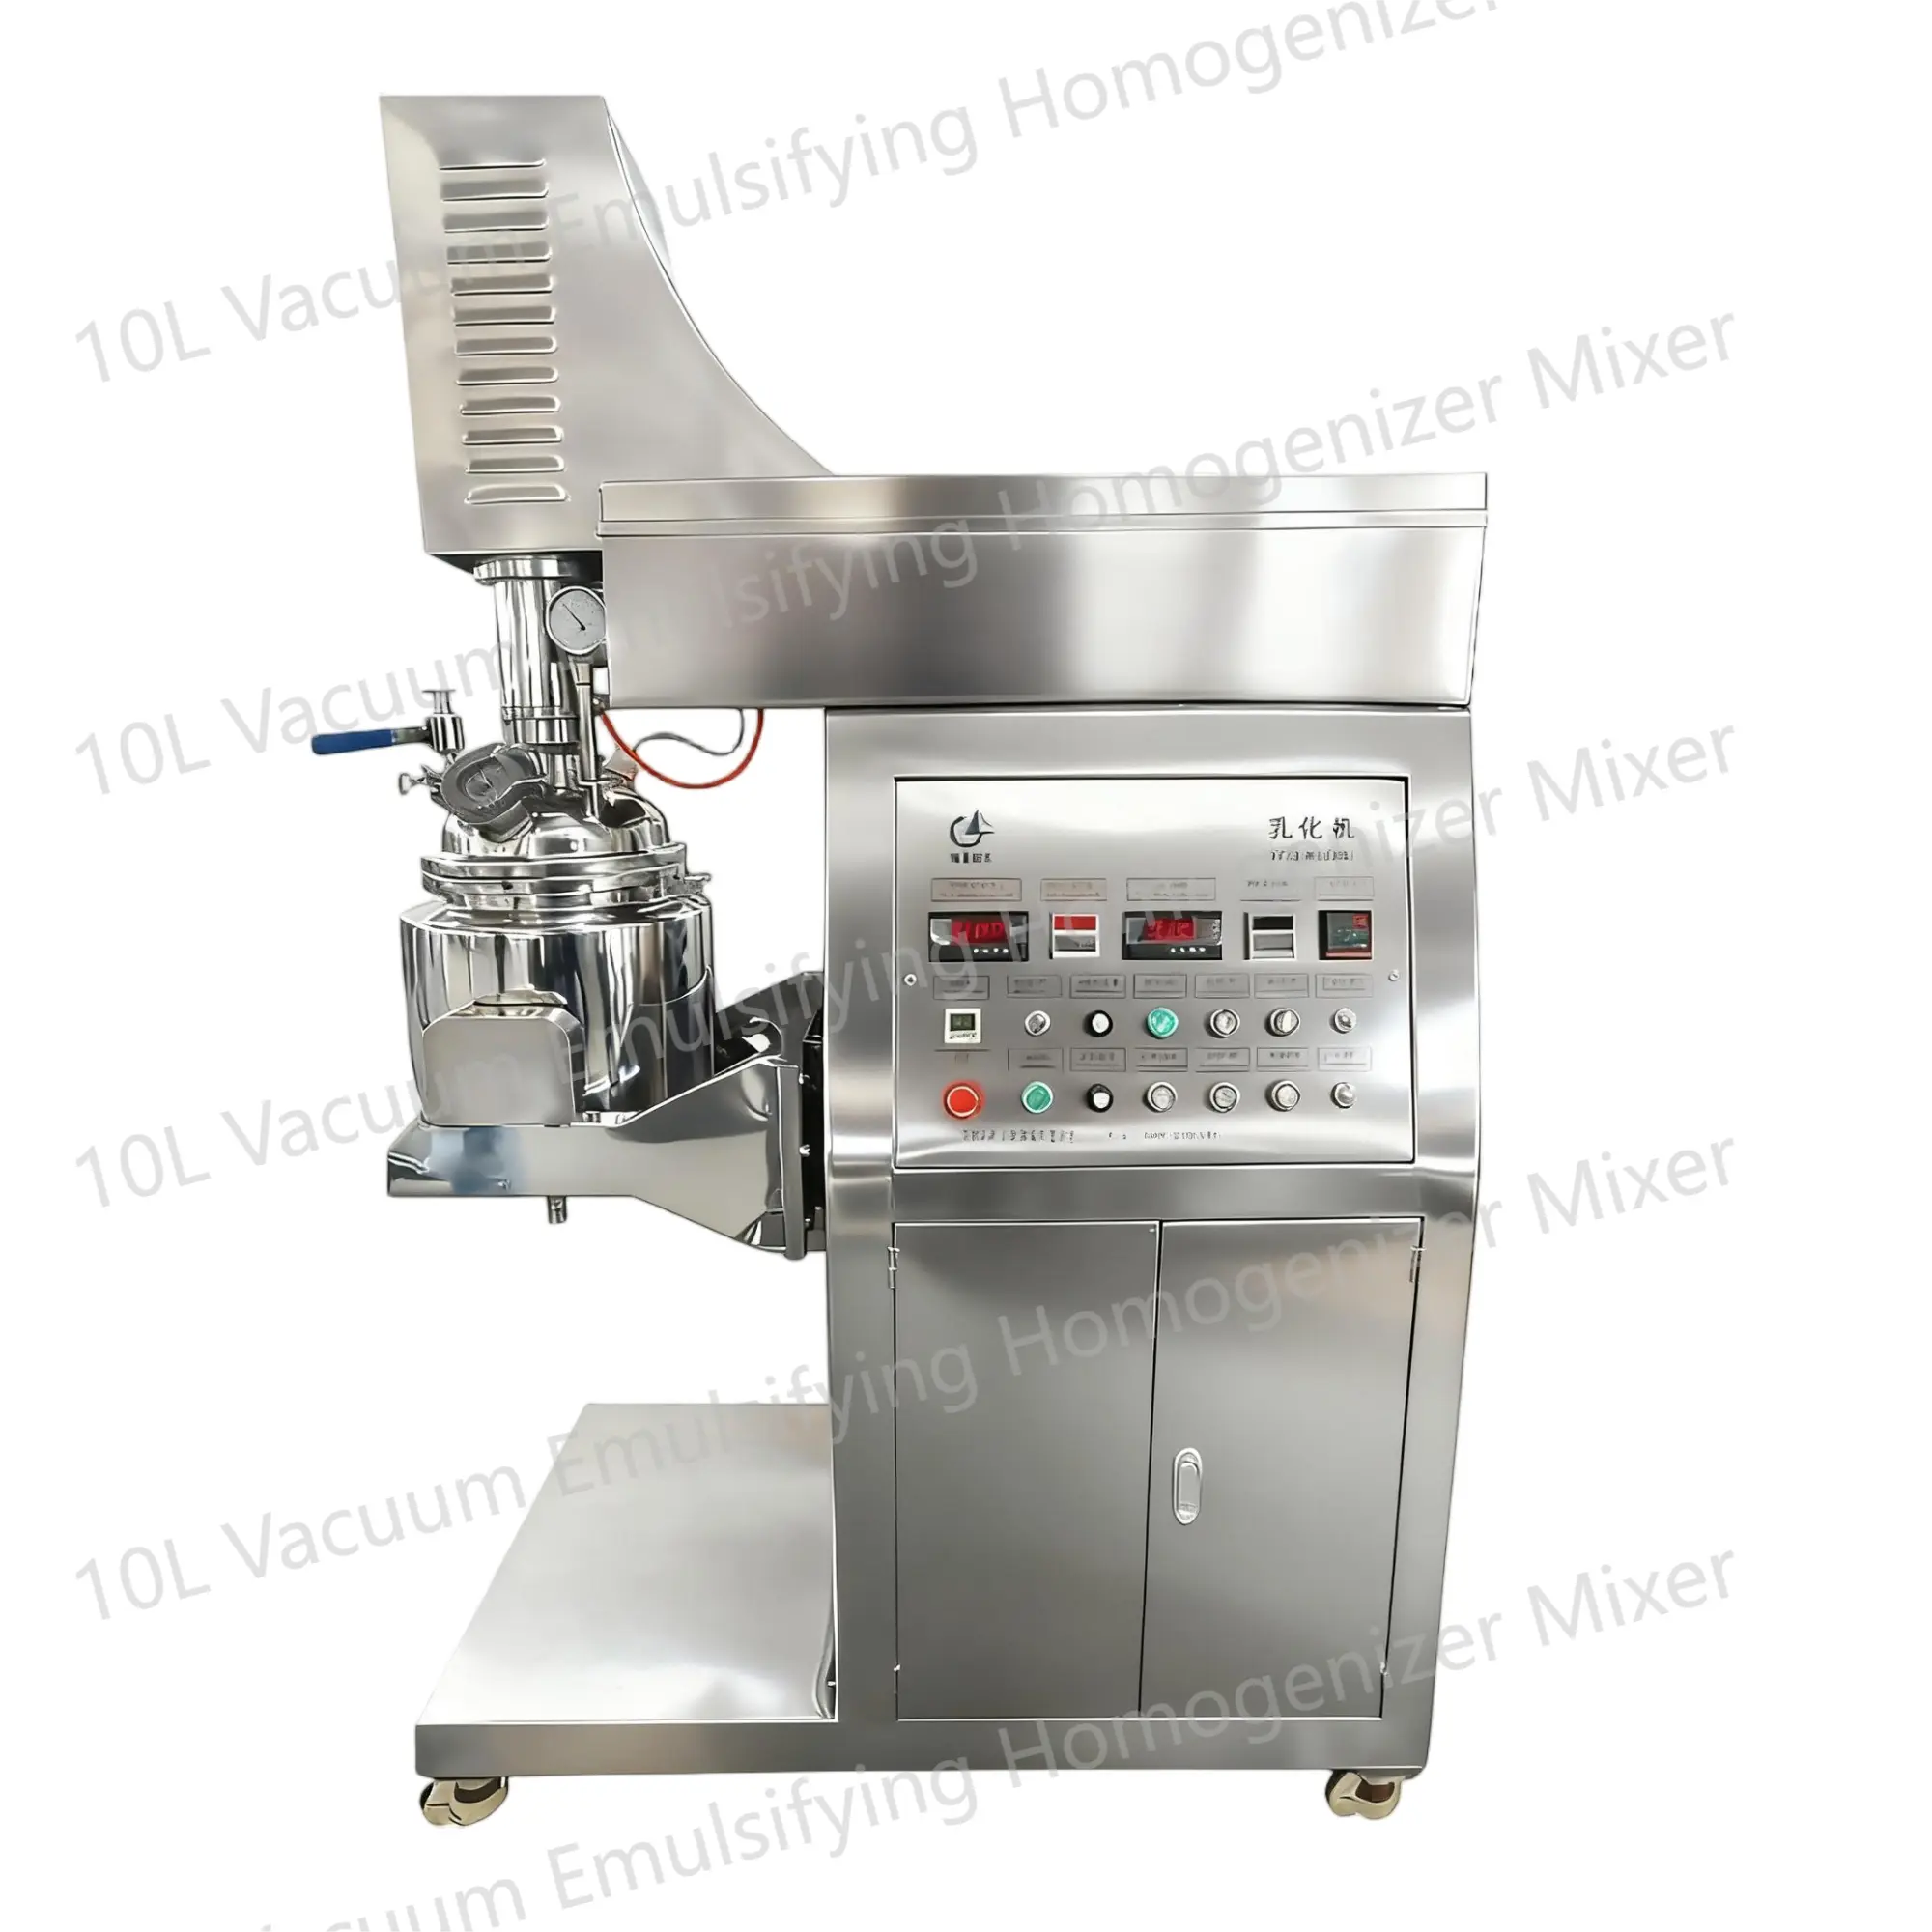 10L Vacuum Emulsifying Homogenizer Mixer
The 10L Vacuum Emulsifying Mixer is a device used for emulsifying and mixing various substances in a vacuum environment. It is commonly used in industries such as food, cosmetics, and pharmaceuticals.